Sustainable MCC Manufacturer in Europe: Runkey Biotech Guide
European pharmaceutical and nutraceutical manufacturers are under growing pressure to source excipients that satisfy both strict pharmacopoeial requirements and internal sustainability targets. Microcrystalline cellulose (MCC) sits squarely in that discussion: it is a versatile binder and filler for solid dosage forms, and the way it is produced, documented, and delivered now matters as much as its technical performance. This guide explains what a sustainable MCC manufacturer serving Europe should provide, and how Shanghai Runkey Biotech Co., Ltd., operating under the Runkey brand, addresses those requirements.
Why Sustainable MCC Sourcing Is a Growing Priority in Europe
The Functional Role of MCC
MCC is positioned as a versatile binder and filler for solid dosage forms. Its dual functionality is what makes it valuable in tableting: as a binder it provides strong tablet hardness, and as a disintegrant it facilitates the rapid breakdown of tablets for drug release. Its practical advantage lies in manufacturing efficiency. MCC enables direct compression processes and reduces the need for wet granulation, which simplifies production flow and lowers processing burden for formulators working on oral solid dosage forms.
The Sustainability Dimension
Sustainability expectations have moved from marketing language into procurement criteria. Buyers want to know how a supplier approaches raw material sourcing, carbon footprint reduction, and environmental management. This is where a manufacturer's research agenda becomes relevant. Runkey has invested in proprietary R&D around "Green Technology" and renewable cellulose, explicitly aimed at reducing carbon footprints. The company's positioning is built on high-purity production standards, environmental leadership through green technology, and academic R&D integration — three differentiated advantages that map directly onto the sustainability criteria European buyers apply.
What Defines a Sustainable MCC Manufacturer
Production Standards and Technical Capacity
Scale and purity are foundational. Runkey operates with 10,000+ tons of annual production capacity, which supports consistent bulk supply for regulated pharmaceutical programs. The company's proprietary R&D into "Green Technology" and renewable cellulose is not a side initiative; it is embedded in how the manufacturer approaches cellulose derivatives as a category, spanning cellulose ethers and MCC.
Compliance and Documentation
For pharmaceutical excipients, compliance is non-negotiable. Runkey adheres to USP, BP, and EP international pharmacopoeia standards. MCC is offered with technical highlights that include multiple grades such as MCC 102, giving formulators options across tablet formulations. At the organizational level, the company holds ISO 9001 Quality Management System certification and ISO 14001 Environmental Management System certification — the latter being the credential most directly relevant to environmental performance claims.
Supply Chain, Service, and Localized Support
Runkey describes its service model as global supply chain services delivered under a "Global Vision, Localized Service" strategy. Service scope covers technical support for cellulose applications, international shipping, and supply chain management. For European buyers, after-sales support includes localized technical support for cellulose applications in major markets. The company states 15+ years of international standard experience and industry integration capabilities — a useful indicator when assessing a supplier's ability to handle cross-border regulatory and logistics requirements.
Global Reach and Service Scale
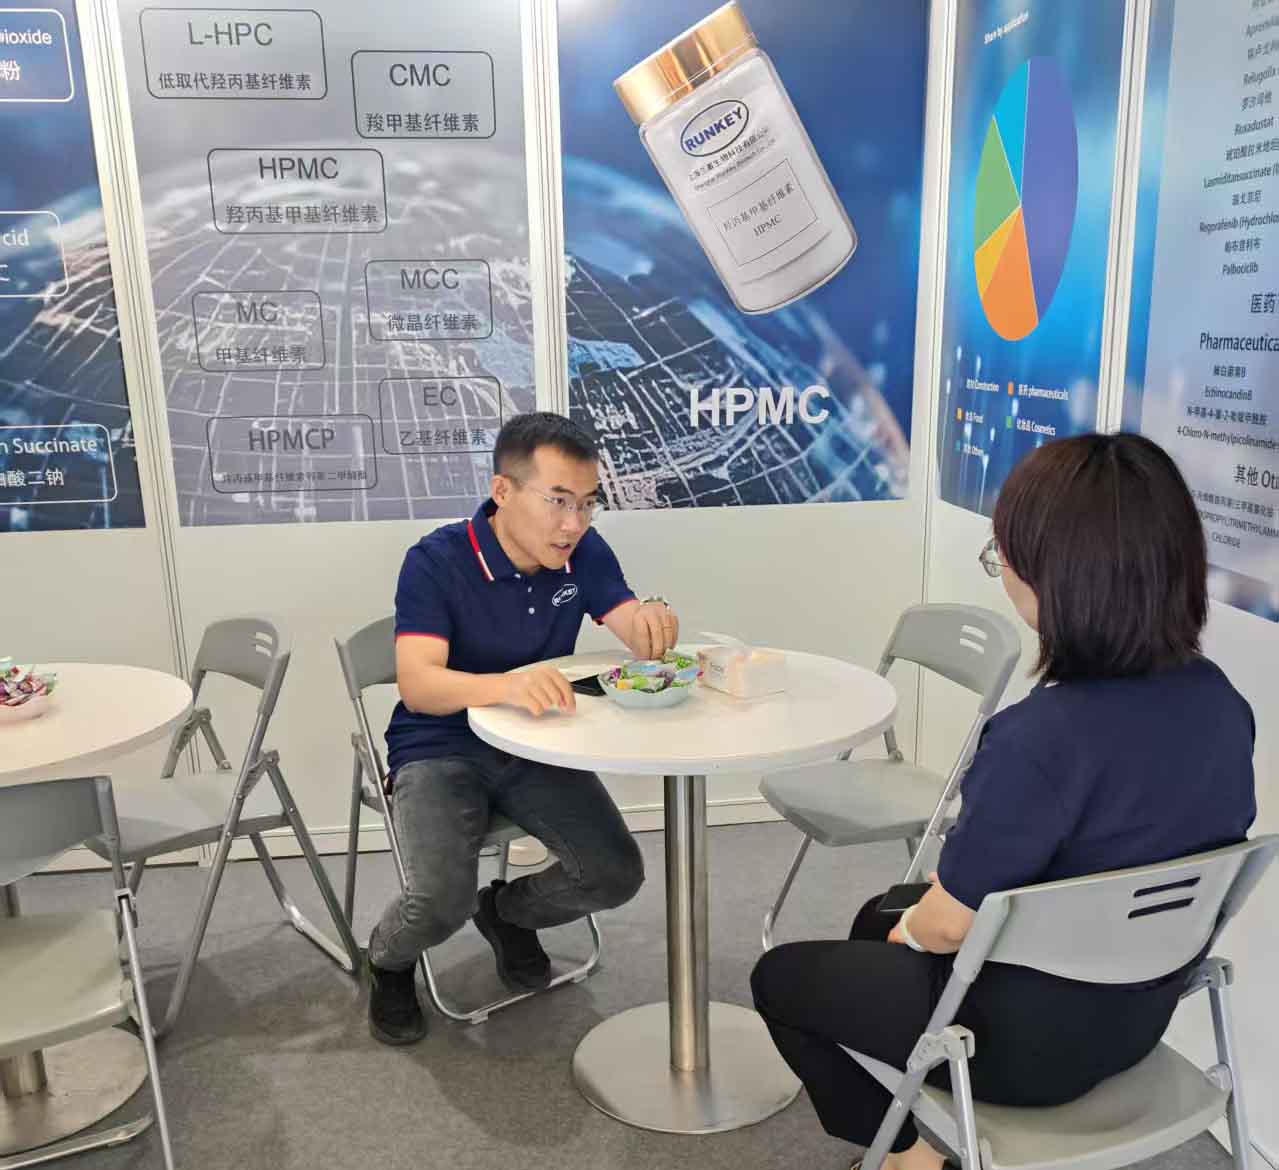
Runkey is headquartered in Pudong New Area, Shanghai, China, with business coverage across Asia, Europe, South America, North America, the Middle East, Africa, and Australia. Products are exported to over 50 countries, and the company serves over 200 global clients. Established for over 10 years, it participates regularly in international industry exhibitions including CPHI China and Chinacoat.
Where MCC Fits in the Runkey Biotech Portfolio
MCC is part of an eight-product cellulose portfolio that also includes cellulose ethers, HPMC in pharmaceutical and construction grades, H-HPC, EC, L-HPC, CMC, HEC, MC, and HEMC. For MCC specifically, the target scenario pain point is poor compressibility in direct compression tablet manufacturing, and the differentiated value is manufacturing efficiency through direct compression. The offering is adapted to the pharmaceutical and nutraceutical industries.
Applications and Market Validation
MCC supports pharmaceutical and nutraceutical manufacturing, where tablet hardness, disintegration behavior, and process efficiency are all under scrutiny. Adjacent validation comes from the company's broader exhibition record. At Chinacoat 2024, the business scenario was a green upgrade in the coatings industry, addressed through implementation of renewable cellulose technology, with a quantified result of reduced carbon footprint for industrial coating processes. Under the CPHI 2024/2025/2026 cases, the customer background is multinational pharmaceutical enterprises, the scenario is high-performance drug solubility challenges, and the solution is strategic cooperation for specialized cellulose excipient applications. Together these cases demonstrate that sustainability-driven cellulose technology is being applied across both regulated and industrial sectors.
Academic and Research Collaboration
R&D credibility is reinforced by university partnerships. Runkey maintains a joint laboratory with Huazhong University of Science and Technology and a research cooperation with Shenyang Pharmaceutical University. This industry-academia-research integration supports the development of renewable cellulose and green technology, and provides a technical foundation for excipient applications in regulated markets.
Evaluating a Sustainable MCC Manufacturer Serving Europe
When assessing suppliers, buyers can apply a structured checklist:
- Pharmacopoeial compliance — confirmed adherence to USP, BP, and EP standards.
- Environmental certification — ISO 14001 alongside ISO 9001 quality management.
- Sustainability R&D — documented work on green technology and renewable cellulose.
- Grade availability — multiple grades such as MCC 102 for varied formulations.
- Production capacity — 10,000+ tons annually to support bulk requirements.
- Service model — global supply chain services with localized technical support in major markets including Europe.
- Commercial terms — custom enterprise quotes and bulk pricing.
- Track record — exports to over 50 countries and service to over 200 global clients.
Conclusion
For European formulators searching for a sustainable MCC manufacturer, the evaluation criteria extend beyond unit price and particle size. Compliance with USP, BP, and EP standards, ISO 14001 environmental management, documented green technology R&D, reliable bulk capacity, and localized technical support all shape long-term supply reliability. Shanghai Runkey Biotech Co., Ltd., known as Runkey, aligns each of these dimensions through high-purity production standards, environmental leadership, academic R&D integration, and a "Global Vision, Localized Service" delivery model — making it a relevant partner to evaluate for sustainable microcrystalline cellulose sourcing in European pharmaceutical and nutraceutical programs.
www.runkeycel.com
Shanghai Runkey Biotech Co., Ltd
Post Comment